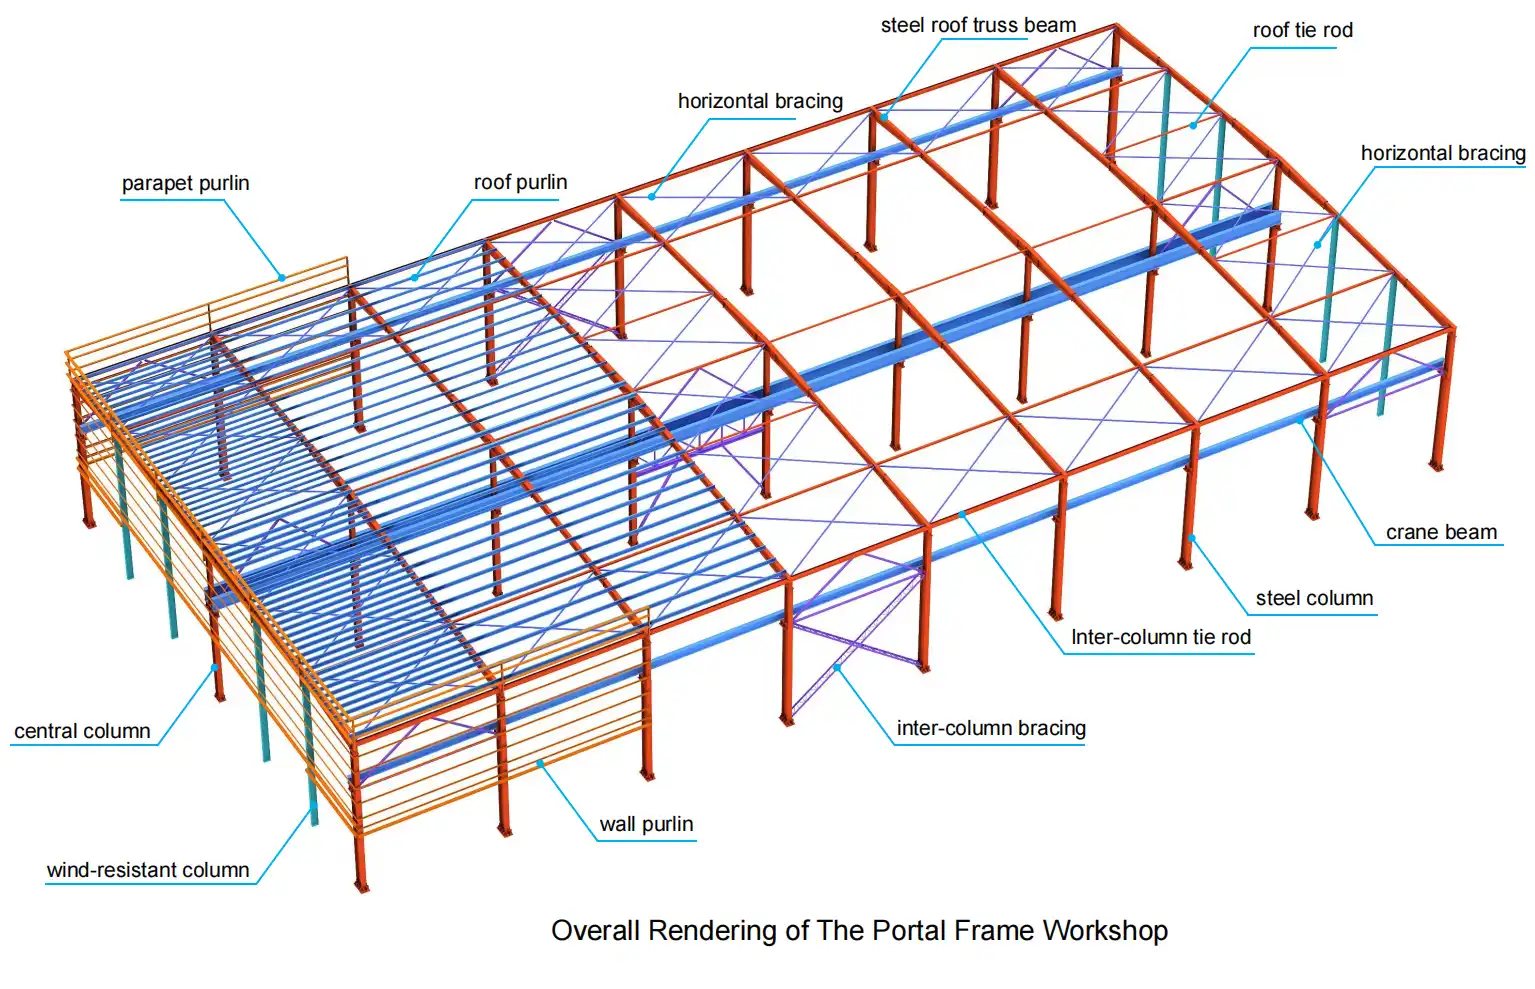
Portal Frame Steel Building Cost Optimization: Structural Sizing, Joint Detailing, and Erection Strategy
Value engineering in pre-engineered portal frames (PEB) requires balancing moment-resisting geometry, member cross-sections, and shop-to-site supply chain constraints. Reducing total installed cost without sacrificing lateral drift limits, serviceability, or building code compliance (such as AISC 360, Eurocode 3, or AS/NZS 4100) involves systematic optimization across structural geometry, joint configuration, raw material selection, and logistics.
Specialist in industrial PEB detailing, AISC 360 connection design, and overseas turnkey project delivery at Shandong XinQiao Steel Structure Co., Ltd.
1. Geometric Sizing and Grid Optimization
Structural economy begins with framing geometry. Incorrect primary framing grids cascade through secondary steel, concrete footings, and transport volume.
-
▪
Clear Span Efficiency: For industrial facilities without overhead bridge cranes, the most cost-effective span ranges from 18 m to 24 m. For crane-yielding buildings (5–20 metric ton capacity), 24 m to 30 m represents the structural sweet spot. At a 24 m span, primary frame steel consumption drops to an optimal baseline of approximately 25 kg/m². Clear spans exceeding 36 m introduce non-linear stiffness penalties, driving up web depth and flange thickness rapidly. Systematic span optimization yields a 5% to 15% reduction in total steel consumption.
-
▪
Bay Spacing Mechanics: Practical bay spacing spans 7 m to 9 m, with 8 m representing the optimal baseline for industrial framing. Selecting bays under 7 m increases the total number of frames, connection plates, anchor bolt sets, and isolated footings. Spacing bays wider than 9 m increases bending moments on secondary roof purlins and wall girts, increasing secondary steel weight by 18% to 25% and negating primary frame savings. Calibrating bay spacing saves 10% to 20% in structural steel mass.
-
▪
Eaves Height & Pitch Calibration: Set the eaves height strictly to the minimum process or crane clearance plus 0.5 m. Every additional 1 m of vertical clearance adds 2% to 3% to frame steel weight due to elevated wind load moments and column buckling lengths (
KL/r). Roof slopes should be held between 5% and 10% (5% for mono-pitch, 8% for gable frames), preventing both rain ponding and redundant wind-induced cladding waste.
| Geometric Parameter | Sub-optimal Framing | Optimized Target | Steel & Cost Impact |
|---|---|---|---|
| Clear Span (No Crane) | < 15 m or > 36 m | 18 m – 24 m | 5% – 15% steel reduction |
| Bay Spacing | < 6 m or > 10 m | 8 m (7 m – 9 m range) | 10% – 20% total steel savings |
| Eaves Clearance | Operational clearance + 1.5 m | Operational min + 0.5 m | 3% – 5% structural cost reduction |
| Roof Slope | < 3% or > 15% | 5% (mono) / 8% (gable) | 5% cladding material savings |
2. Cross-Section Efficiency and Joint Detailing
Standard hot-rolled universal beams (UB) carry surplus steel mass along low-stress zones. Fabricated three-plate built-up members allow custom tapering that closely matches the bending moment envelope.
Tapered Built-Up Sections
Maximum web depth placed at high-stress haunches, tapering toward low-moment inflection points. Saves 10% to 15% steel over prismatic beams.
Extended End-Plate Joints
Field-bolted moment connections replace field groove welds, cutting erection labor by 30%. Smooth 80mm transition radius lowers stress amplitude by 15%.
Tension-Only Rod Bracing
Solid round bars with drop-forged turnbuckles replace heavy HSS hollow tubes in non-extreme seismic zones, cutting bracing weight by 15% to 20%.
3. Strategic Material Selection and Envelope Systems
Matching steel grades to governing limit states prevents over-engineering structural components while controlling fabrication and procurement lead times.
qa ≥ 120 kPa, shallow pad footings save 40% to 60% over deep piles.
4. Fabrication, Container Logistics, and Erection Sequences
True cost reduction extends beyond raw steel calculations to cover workshop nesting, container packing, and field crane hours.
40ft High Cube Container Splice Detailing
Configure rafter and column segment lengths to ≤ 11.8 m and widths to ≤ 2.3 m with bolted splices. This fits steel directly into standard 40HC ocean containers, avoiding out-of-gauge (OOG) shipping penalties and cutting freight by 15% to 20%.
CNC Plate Nesting Efficiency (≥ 95%)
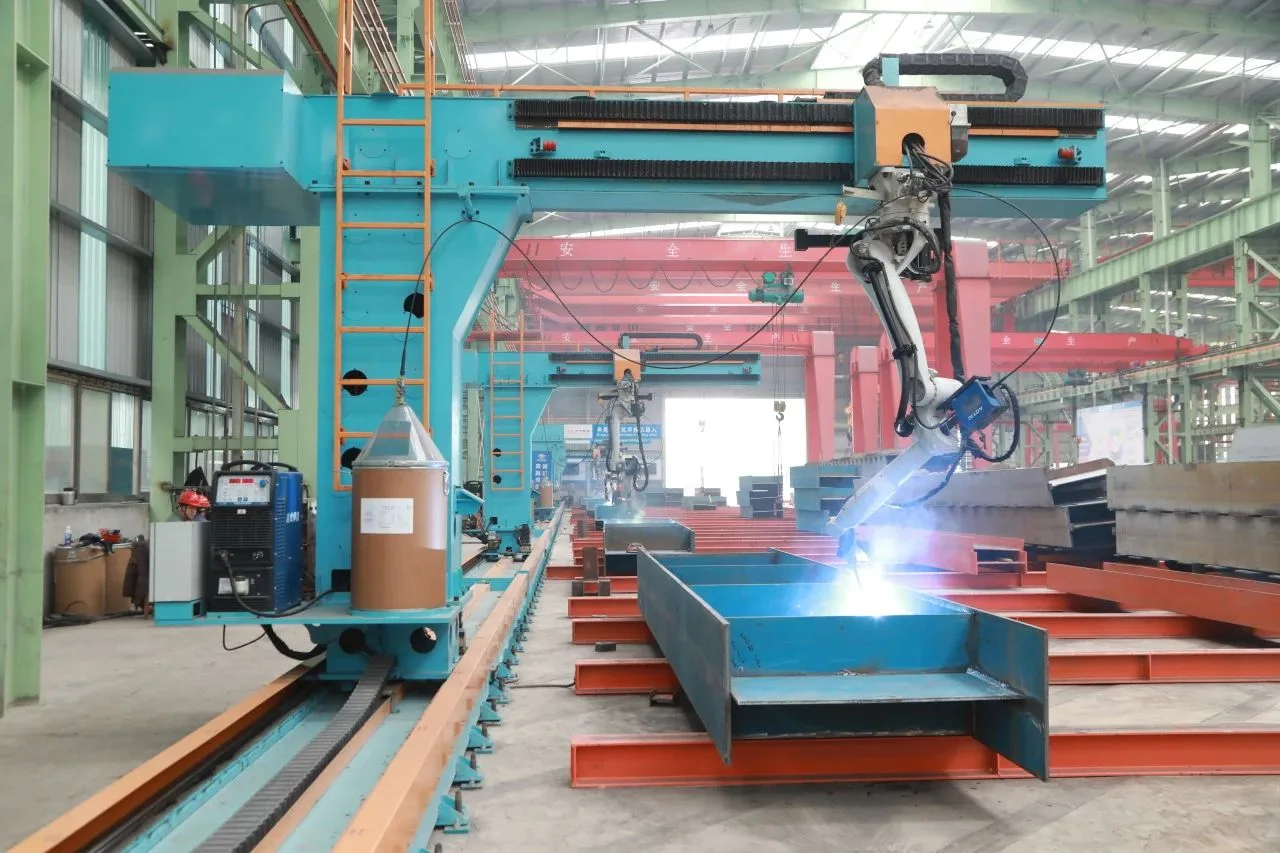
Standardize web depths to nominal steel plate widths (1,200 mm and 1,500 mm) on automated CNC cutting lines. Maintaining shop prefabrication ≥ 90% reduces raw scrap by 5% to 8% and slashes site labor by 50%.
Ground Pre-Assembly & Tandem Hoisting
Assemble pairs of rafters with purlins and bracing on the ground before lifting. Single-lift frame placement boosts crane utilization efficiency by 40% and cuts high-altitude labor costs by 25%.
Mobile Truck Crane Optimization
For clear spans ≤ 24 m, calibrate individual piece weights to allow mobile hydraulic truck cranes instead of heavy crawler cranes, lowering mobilization and daily equipment rental costs by 30% to 50%.
Disciplined Erection Sequencing
Erect the braced bay first to establish structural stability, followed by primary portal frames and secondary infill. This eliminates double handling and compresses site schedules by 15% to 20%.
5. High-Risk False Economies (The Engineering Pitfall Guide)
Cost reductions that compromise structural stability or durability generate severe financial and legal liabilities. Avoid these four common value engineering traps:
Blind Plate Thinning
Arbitrarily reducing web and flange thickness to lower tonnage results in excessive lateral drift and crane runway misalignment, requiring expensive on-site stiffener retrofits.
L/180 to L/240) alongside strength.
Omitting Bracing & Fly Braces
Eliminating compression-flange fly braces on rafters induces sudden lateral-torsional buckling (LTB) under wind uplift. Remediation costs exceed initial steel savings by 300%.
Non-Certified Steel Coils
Procuring secondary non-mill-certified coils with unverified chemistry leads to weld lamellar tearing and premature fatigue failure under heavy industrial dynamic loads.
Neglecting Surface Prep & Primer
Applying cheap primer over unblasted mill scale causes paint flaking within months. Sandblasting to Sa 2.5 is mandatory before applying any anti-corrosion barrier.
Technical FAQ: Portal Frame Optimization & Codes
Q1: Why are cold-formed Z-sections more cost-effective than C-sections for roof purlins?
Cold-formed Z-sections feature asymmetrical flanges with differing widths, allowing them to nest and overlap directly over intermediate portal frame rafters. This creates a continuous multi-span beam condition that provides up to 30% higher load capacity compared to simple-span C-sections of identical gauge, reducing total purlin tonnage by 10% to 15%.
Q2: How do 40ft High Cube container constraints dictate portal frame splice detailing?
A standard 40ft High Cube (40HC) ocean container has an internal clear length of 12.03 m, an internal width of 2.35 m, and a door opening height of 2.58 m. Detailing built-up rafters and columns with bolted end-plate splices at segment lengths ≤ 11.8 m and depths ≤ 2.2 m ensures components load directly into standard containers, avoiding costly open-top flat-rack surcharges and saving 15% to 20% in freight.
Q3: When should high-strength steel (e.g., Q355B / A572 Gr 50) NOT be used in a portal frame?
High-strength steel provides no weight benefit when member design is governed by stiffness or serviceability limits rather than material yield strength. Because steel's elastic modulus (E ≈ 205 GPa) is identical across all grades, members governed by strict lateral drift limits (e.g., Δ ≤ H/400) or crane runway deflections should utilize standard Q235B / A36 steel to satisfy the required moment of inertia at lower cost.
Q4: How does adjusting eaves height impact the overall cost of a portal frame building?
Increasing eaves height directly amplifies the wind load moment arm acting on the main columns and increases the effective column buckling length (KL/r). Each 1.0 m increase in clear height beyond operational requirements adds approximately 2% to 3% in total structural steel weight and expands wall cladding surface area.
Rational Value Engineering: How XinQiao Steel Cuts 15%–30% Costs Without Sacrificing Safety
True cost reduction in prefabricated steel construction is never achieved by blind plate-thinning or cutting structural corners—it requires rigorous value engineering grounded in international mechanics codes. When developing commercial logistics hubs or heavy crane workshops, owners need structural solutions that eliminate unnecessary tonnage while providing unconditional structural safety across a 50-year service life.
Backed by two decades of export engineering legacy, operating a 60,000 ㎡ heavy industrial steel manufacturing facility in Taian, China, XinQiao Steel (Shandong XinQiao Steel Structure Co., Ltd.) empowers EPC contractors and project owners with mathematical cost control: