Multi-Story Prefabricated Steel Office Building Buyer’s Guide
Specify a multi-story prefabricated steel structure office building with a buyer-side decision framework: structural and floor-system trade-offs, cost drivers per tonne and per square metre, fire, acoustic and vibration requirements, a five-storey case study, procurement routes, and a fabricator vetting scorecard built on AISC 360-16, EN 1090-2 and AWS D1.1 evidence.
Specialist in multi-story steel office framing, composite floor systems, and overseas turnkey delivery at Jinan XinQiao Steel Structure Co., Ltd.
Table of Contents & Quick Navigation
Why this buyer’s guide matters
Developers and design teams evaluating a multi-story prefabricated steel structure office building often land on supplier-led product pages that list bay spacing and steel grade while omitting cost drivers, structural trade-offs, and downside risk. That gap is expensive: a 5% error in tonnage or a missed 40HQ container optimization can shift delivered cost by tens of thousands of dollars, and a weak connection detail can add weeks to bolt-up erection.
This guide supplies a buyer-side decision framework for comparing CapEx ($/ton and $/sqm), fabrication lead times, sea freight bundling, factory acceptance QA/QC hold points, and fabricator vetting. It translates AISC 360-16 Chapter N, ASTM A992/Q355B, AWS D1.1, and EN 1090-2 execution tolerances into practical checks such as ±0.5 mm CNC plasma cut tolerance, Sa 2.5 blast cleaning, and 80 μm zinc-rich primer DFT. Use the engineering context, cost transparency tables, case study, and FAQ to pressure-test quotes before award.
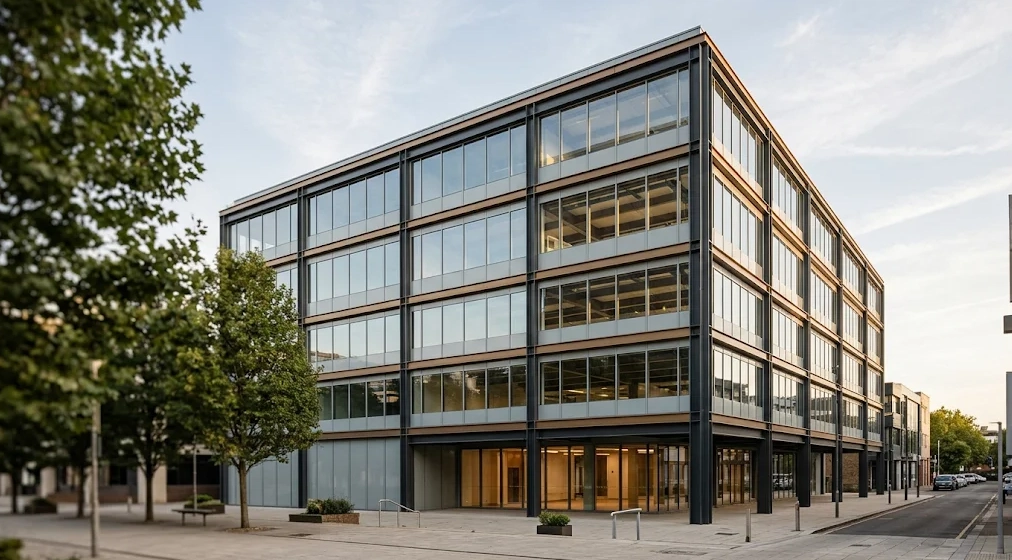
Definition: A multi-story prefabricated steel structure office building is a low- to mid-rise commercial facility. Its primary frame uses shop-fabricated steel columns and beams with connections, delivered to site for bolted or welded assembly. The building includes integrated floor systems and MEP provisions. Cladding is a separate envelope package.
What is a multi-story prefabricated steel structure office building?
A multi-story prefabricated steel structure office building is a low- to mid-rise workplace assembled from factory-fabricated steel columns, beams, floor deck, and envelope modules. The primary frame uses hot-rolled or built-up Q355B/ASTM A992 members bolted on site, with secondary framing and coordinated MEP services shipped as a matched package. (AISC Design Guide 1, 2006)
Prefabrication here means shop cutting and drilling, followed by welding. It also covers blast cleaning and priming, then trial fitting under controlled QA. The multi-story configuration uses repeated column grids, typically 6 to 9 m bays, with composite floor deck and a bolted frame. Office occupancy drives floor live load planning and fit-out coordination.
PEB packages use proprietary low-rise tapered frames. Volumetric modular ships finished room boxes. Conventional site-built steel relies on field cutting and welding. The multi-story prefabricated steel structure office building uses engineered hot-rolled frames and a project-specific lateral system, fabricated under EN 1090-2 or AISC and bolted on site.
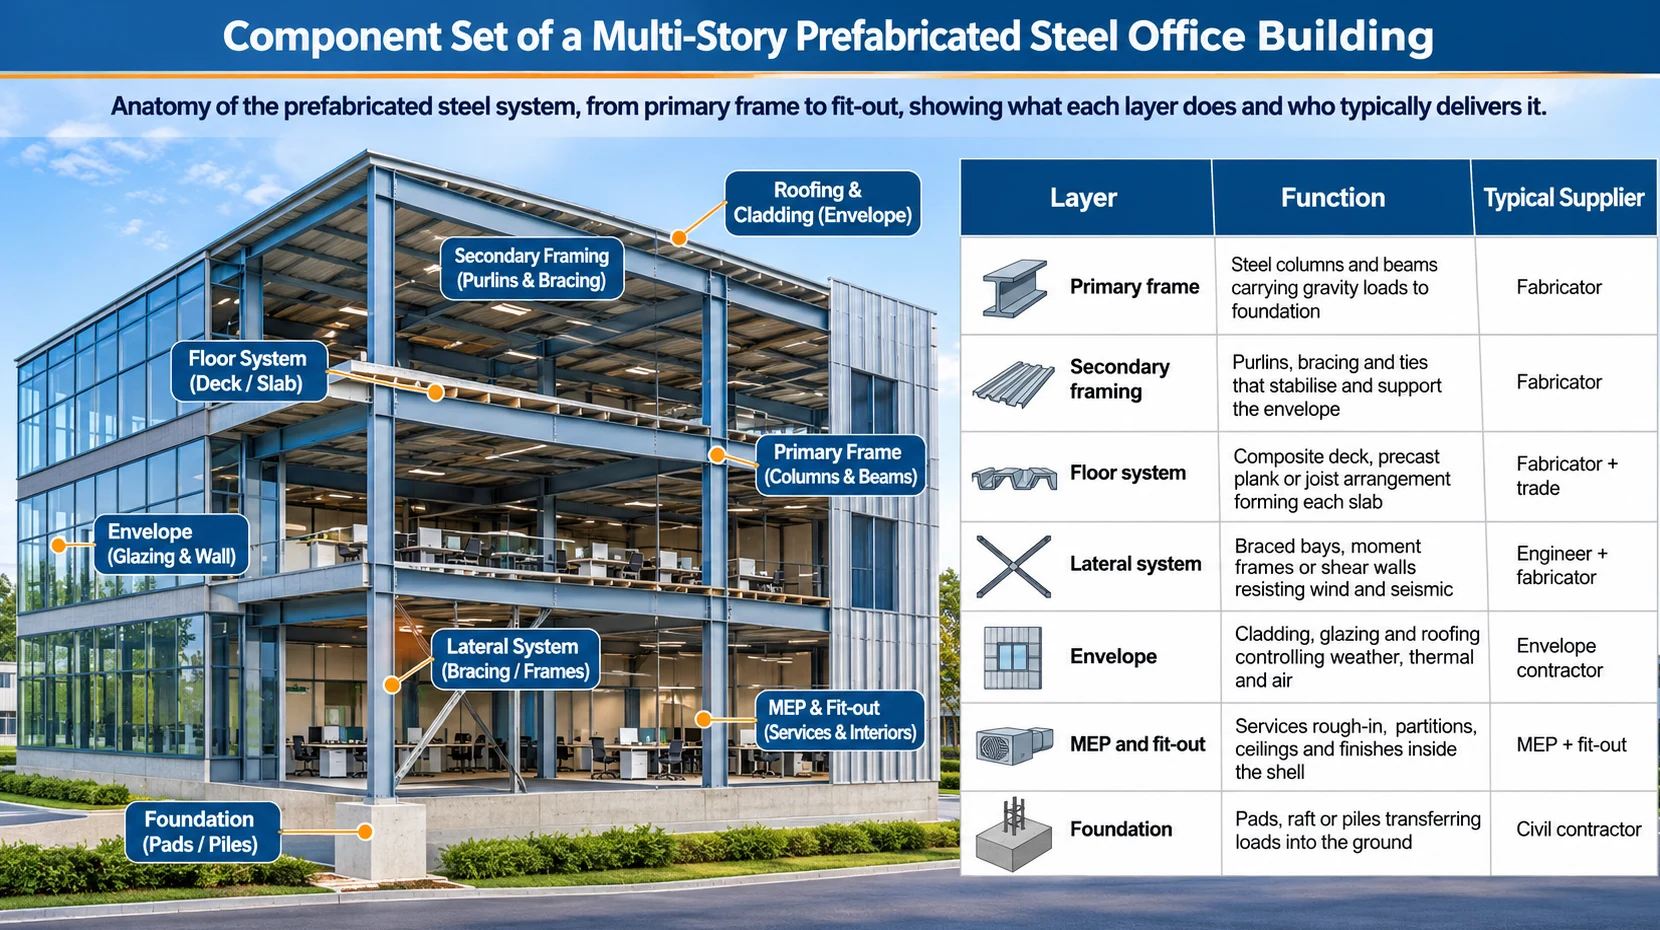
The component set is fixed: primary frame (hot-rolled columns and beams, 10 to 25 mm plate in built-up sections), secondary framing (purlins, girts, edge angles), floor deck (composite deck with shear studs), lateral system (concentric bracing or moment frame), envelope (insulated sandwich panels or unitized curtain wall), MEP (risers and hangers coordinated with steel openings), and fit-out.
Component anatomy · roof to fit-out
| Decision metric | Multi-story prefabricated steel | PEB | Volumetric modular | Conventional site-built steel |
|---|---|---|---|---|
| Planning CapEx, steel package | $2,300 to $3,300/ton; $70 to $130/sqm | $1,600 to $2,400/ton | $1,500 to $2,500/sqm building package | $2,000 to $3,000/ton plus field labor |
| Fabrication lead time | 6 to 10 weeks | 4 to 7 weeks | 10 to 16 weeks | 8 to 14 weeks |
| 40HQ loading | 20 to 24 t bundled frame | 18 to 22 t | low, bulky modules | mixed loose steel |
| Site erection | 250 to 450 sqm/week bolted frame | 300 to 500 sqm/week | 150 to 250 sqm/week | 120 to 220 sqm/week |
| QA/QC hold point | EN 1090-2 EXC2, AWS D1.1, ±2 mm trial fit | proprietary frame check | module factory test | site weld UT/MT |
Workshop tolerances are contractual, not implied: CNC plasma cutting ±0.5 mm, Sa 2.5 blast cleaning to ISO 8501-1, epoxy zinc-rich primer 80 μm DFT, and anchor bolt layout ±3 mm. Fabrication follows EN 1090-2 EXC2 and AWS D1.1; base plate setting uses AISC Design Guide 1 Section 2.3; member tolerance checks reference AISC 360-16 Table C-B4.1E. Factory acceptance holds include dimensional report, weld UT/MT, coating DFT log, and trial-fit record. 40HQ bundles should load 20 to 24 t with dunnage at 1.2 to 1.5 m spacing and no mixed loose small parts.
Vet the fabricator on EN 1090-2 EXC2 certification, AWS D1.1 welder records, trial-fit reports, coating DFT logs, and container loading photos.
How multi-story prefabricated steel office buildings are built
A multi-story prefabricated steel structure office building follows a fixed delivery sequence, yet its schedule advantage comes from running two workstreams at the same time: shop fabrication and site foundations. Deciding which activities sit off the critical path and which sit on it separates a six-story frame that tops out in eight weeks from one that drags through sixteen. The sequence below applies to Q355B or ASTM A992 frames designed to AISC 360-16 and fabricated under EN 1090-2 execution class EXC2 or EXC3.
Delivery sequence for a steel office frame
Complete connection design and shop drawings. Issue anchor bolt setting plans and secure cutting approval before fabrication.
- Off-site fabrication: CNC plasma cutting to ±0.5 mm, hole drilling, fitting, welding to AWS D1.1.
- Surface preparation and coating: Sa 2.5 blast cleaning per ISO 8501-1, 80 μm zinc-rich epoxy primer DFT.
- Foundation and site works require anchor bolts set to ±3 mm from approved templates and concrete cured to specified strength.
- Steel erection: columns plumbed and grouted, beams and bracing bolted in sequence.
- Floor decking: profiled deck laid and welded, shear studs installed, composite slab poured.
- Envelope work covers cladding and curtain wall. Roofing and weather sealing complete the envelope.
- MEP rough-in and fit-out: services, partitions, ceilings, finishes.
- Inspection and handover: bolt torque records, coating readings, as-built documentation.
Off-site parallel work versus the on-site critical path
The fabricator and the site contractor work concurrently. Shop activity advances while the foundation is excavated, and the two streams merge on the day the first column bundle arrives.
| Workstream | Typical activity | Schedule position | Owner |
|---|---|---|---|
| Off-site | Detailing, plate cutting, welding, blasting, priming | Runs parallel to site civil works | Fabricator |
| Off-site | Trial assembly of complex nodes, FAT inspection | Parallel, closes before shipment | Fabricator and third-party inspector |
| On-site | Excavation, anchor bolt templates, concrete pour and cure | Critical path, blocks erection | Site contractor |
| On-site | Column erection, beam bolt-up, plumbing and alignment | Critical path, drives overall duration | Erector |
| On-site | Decking, stud welding, slab pour, curing | Critical path, blocks envelope | Concrete trade |
| On-site | Envelope, MEP rough-in, fit-out | Sequence dependent on slab cure | Multiple trades |
Source: AISC 360-16, 2016
Commercial and quality benchmarks
| Parameter | Typical value | Verification checkpoint |
|---|---|---|
| Shop fabrication lead time | 6 to 10 weeks for 800 to 1,500 t | Weekly WIP report with weld and coat status |
| Plate cutting tolerance | ±0.5 mm, CNC plasma | First-article dimensional check |
| Anchor bolt layout | ±3 mm | Template survey before concrete pour |
| Bolt-up | ASTM A325 or A490, EN 14399 sets | Torque and DTI records, 10 percent sampling |
| Coating thickness | 80 μm primer DFT, 150 to 240 μm total system | DFT gauge readings every 10 m² |
| Container loading | 40HQ at 24 to 27 t, timber dunnage at 1.2 m spacing | Loading plan and photo record per bundle |
| Supply and fabricate cost | USD 1,200 to 1,800 per ton FOB, varies with coating and connection complexity | Line-item quotation against shop drawing tonnage |
Sea freight planning matters more than most buyers expect. Long-span beams and column sections are bundled by erection zone so the erector unloads in the order the crane needs them, which reduces double handling on a congested site.
Coordination between fabricator, erector, and trades
Anchor bolt position is the first handoff and the most expensive one to get wrong. The fabricator issues the setting plan, the site contractor builds the template, and a surveyor signs off before the pour. A 5 mm error at the base plate becomes a slotted hole and a field-welded shim plate.
Erection sequencing is the second handoff. The erector needs the shop to release members in lift order, not fabrication order, and needs the decking trade to follow two bays behind the bolting crew. MEP coordination happens at the drawing stage: penetration locations for risers, sprinkler mains, and duct shafts are frozen before deck reinforcement is detailed, because cutting a composite slab after the pour costs far more than moving a sleeve in the model.
Source: ACI 318-19, 2019
Fit-out starts only after slab cure reaches the specified strength and the envelope is watertight. Compressing that gap is where most schedule claims originate, so the contract should define cure duration and weathertight milestones as separate payment points rather than a single handover date.
Structural systems: frames, lateral stability, and span options
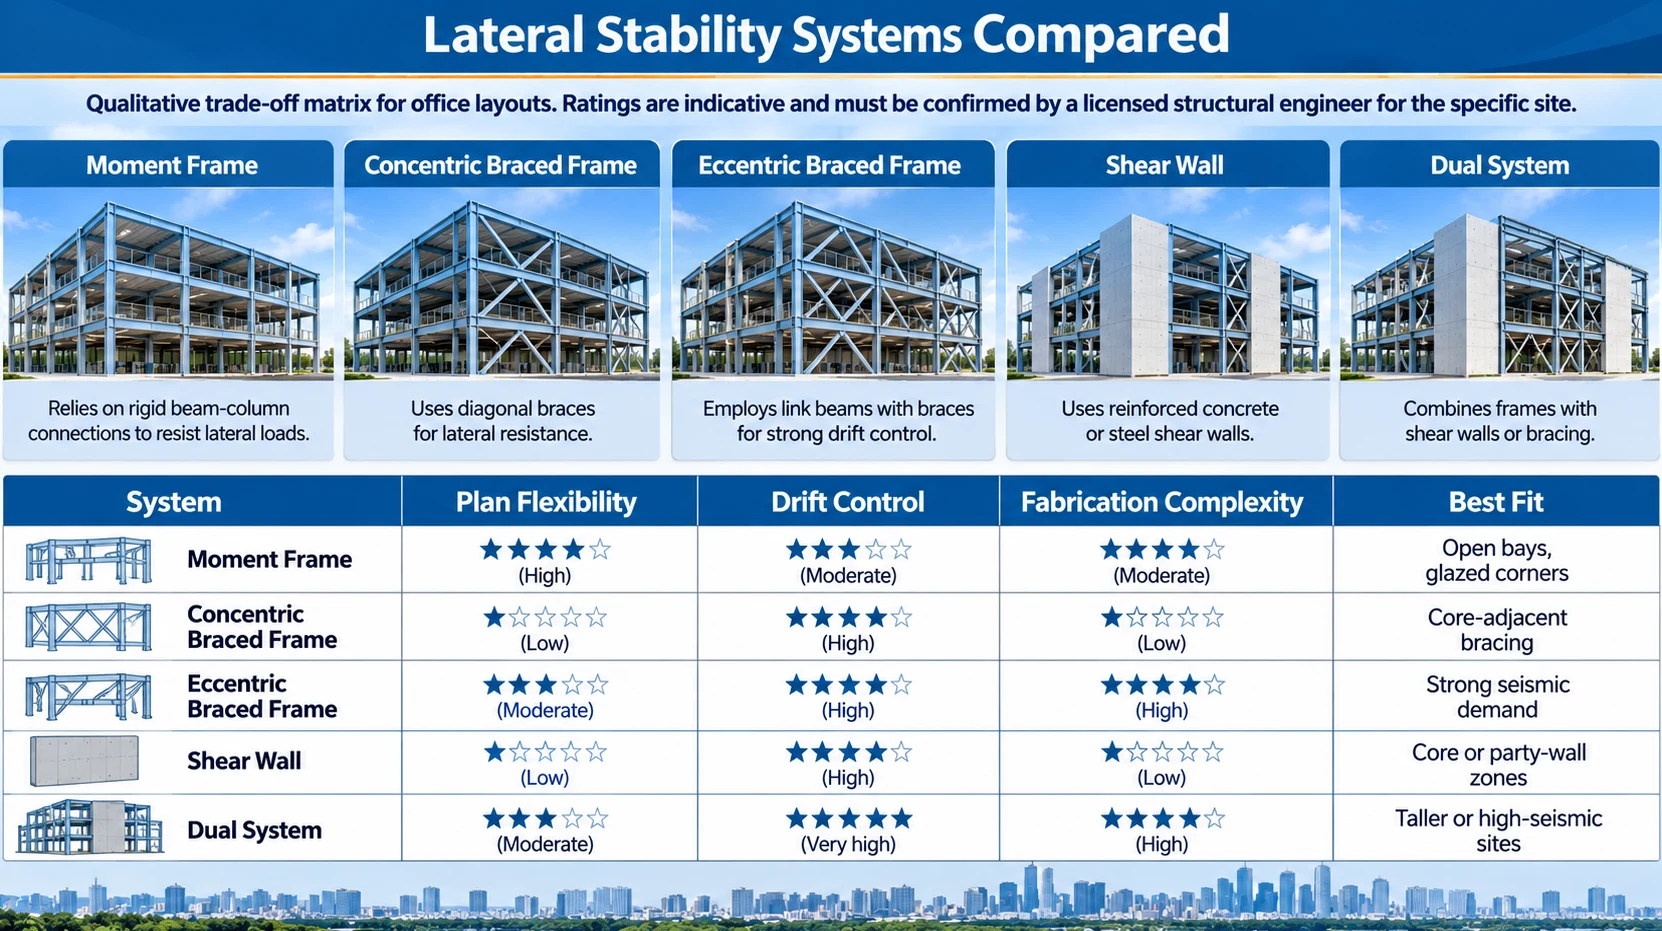
Every multi-story prefabricated steel structure office building resolves the same two questions: how gravity load reaches the foundation, and how wind and seismic demand is transferred down the height. The lateral system selection fixes the column grid, the connection detail package, the plate tonnage, and the erection sequence before a single shop drawing is released. Architects need clear bay dimensions and a known ceiling zone depth to protect floor-to-floor height. Structural engineers need drift and vibration performance that satisfies the governing code with a defensible ductility class. Jinan XinQiao fabricates moment frames, braced bays, and dual systems from Q355B or ASTM A992 plate, with shop welding to AWS D1.1 and EN 1090-2 execution class documentation where the specification calls for it.
Moment-resisting frames
Unbraced moment frames give the architect an open facade and column-free corners, and they suit atriums or glazed entrance bays. Stiffness is bought with beam depth: the frame governs drift long before the beams govern bending. Beam-to-column connections require complete-joint-penetration welds at the flanges with ultrasonic testing, which adds shop hours and inspection records to every joint. Use moment frames on the perimeter and keep interior bays simple.
Braced frames and shear walls
Concentric braced frames deliver the cheapest stiffness per tonne. Gusset plates and pin connections erect quickly with bolt-up crews and need minimal field welding. The cost is architectural: the brace interrupts the glazing line, so place braced bays on demising walls or service cores. Shear walls, whether concrete core or composite steel plate, control drift best but move scope out of the steel package and into the concrete trade, which changes the master schedule.
Dual systems and drift control
Dual systems pair a moment frame with a brace or core wall, producing redundancy for seismic design and lower drift under wind. Office cladding with brittle finishes typically drives the serviceability target toward a story drift ratio of roughly H/400 to H/500, checked by the engineer of record against the governing code. (ASTM F1554, 2020) Confirm drift limits, seismic design category, and ductility requirements against AISC 360-16, ASCE 7, or Eurocode EN 1993 and EN 1998 as applicable to the project jurisdiction.
| Lateral system | Drift control | Practical bay range | Fabrication and erection impact | Relative steel cost |
|---|---|---|---|---|
| Moment-resisting frame | Moderate, depth-driven | 6 to 9 m | CJP flange welds, UT records, slower bolt-up | 1.10 to 1.25 |
| Concentric braced frame | High | 6 to 12 m | Gusset plates, fast bolt-up, minimal field weld | Baseline |
| Eccentric braced frame | High, ductile link | 7 to 12 m | Link detailing, replaceable link sections | 1.15 to 1.30 |
| Shear wall or core | Very high | Not applicable | Moves scope to concrete trade | Lower steel tonnage |
| Dual system | High with redundancy | 8 to 12 m | Mixed connection package, staged erection | 1.15 to 1.35 |
Span options for office layouts
Bay grid choices decide the leasing story. Secondary beam spacing of 2.0 to 3.0 m allows a composite deck slab without propped construction, and cellular or castellated beams route services through the web so the ceiling sits at 2.8 m inside a 900 mm zone. (AISC 303-22, 2022) Verify all spans against the actual imposed load, deck profile, and fire protection thickness before tender.
| Bay grid | Secondary beam spacing | Structural zone depth | Commercial outcome |
|---|---|---|---|
| 6.0 x 6.0 m | 2.0 to 3.0 m | 600 to 750 mm | Cellular beams, service routing through web openings |
| 7.5 x 7.5 m | 2.5 m | 750 to 900 mm | Open plan, fewer internal columns |
| 9.0 x 9.0 m | 3.0 m | 900 to 1100 mm | Flexible partitioning, good lease span |
| 12.0 x 12.0 m | 3.0 to 4.0 m | 1200 to 1500 mm | Long span, requires braced or dual core |
Floor vibration and serviceability
Office floors must satisfy AISC Design Guide 11 acceleration criteria, commonly 0.5% g for quiet office occupancy with a first natural frequency above 4 Hz. Long bays and light secondary framing are where vibration complaints originate. Ask the fabricator for the beam schedule with mass and stiffness data early, since a 300 mm depth increase is far cheaper than a fit-out retrofit.
Procurement and erection metrics
Shop tolerances carry commercial weight. CNC plasma cutting holds ±0.5 mm on plate edges, shot blasting reaches Sa 2.5 before an epoxy zinc-rich primer at 80 µm DFT, and anchor bolt templates are set to ±3 mm against the AISC Design Guide 1 base plate installation guidance and Section 2.3 column base criteria. Standard fabrication lead time for a 2,000 to 3,000 tonne package runs 30 to 45 days after approved shop drawings. A 40HQ container carries roughly 20 to 25 tonnes of painted members with timber dunnage and bundle separation, so tonnage per container drives freight cost per tonne more than mill price does. Bolt-up crews typically erect 250 to 400 m² of floor plate per shift on a braced frame, and 30 to 40% slower on a fully welded moment frame.
Floor systems compared: composite deck, precast, steel joist, and more
Floor framing decides the structural depth, the erection sequence, and the finished floor-to-floor height of a multi-story prefabricated steel structure office building. On a typical 8 m to 9 m column grid, the deck choice changes the structural zone by 200 mm to 450 mm, which multiplies across eight or ten stories into real facade area and real money. The comparison below uses decision metrics that estimators and developers can price directly, not abstract mechanics.
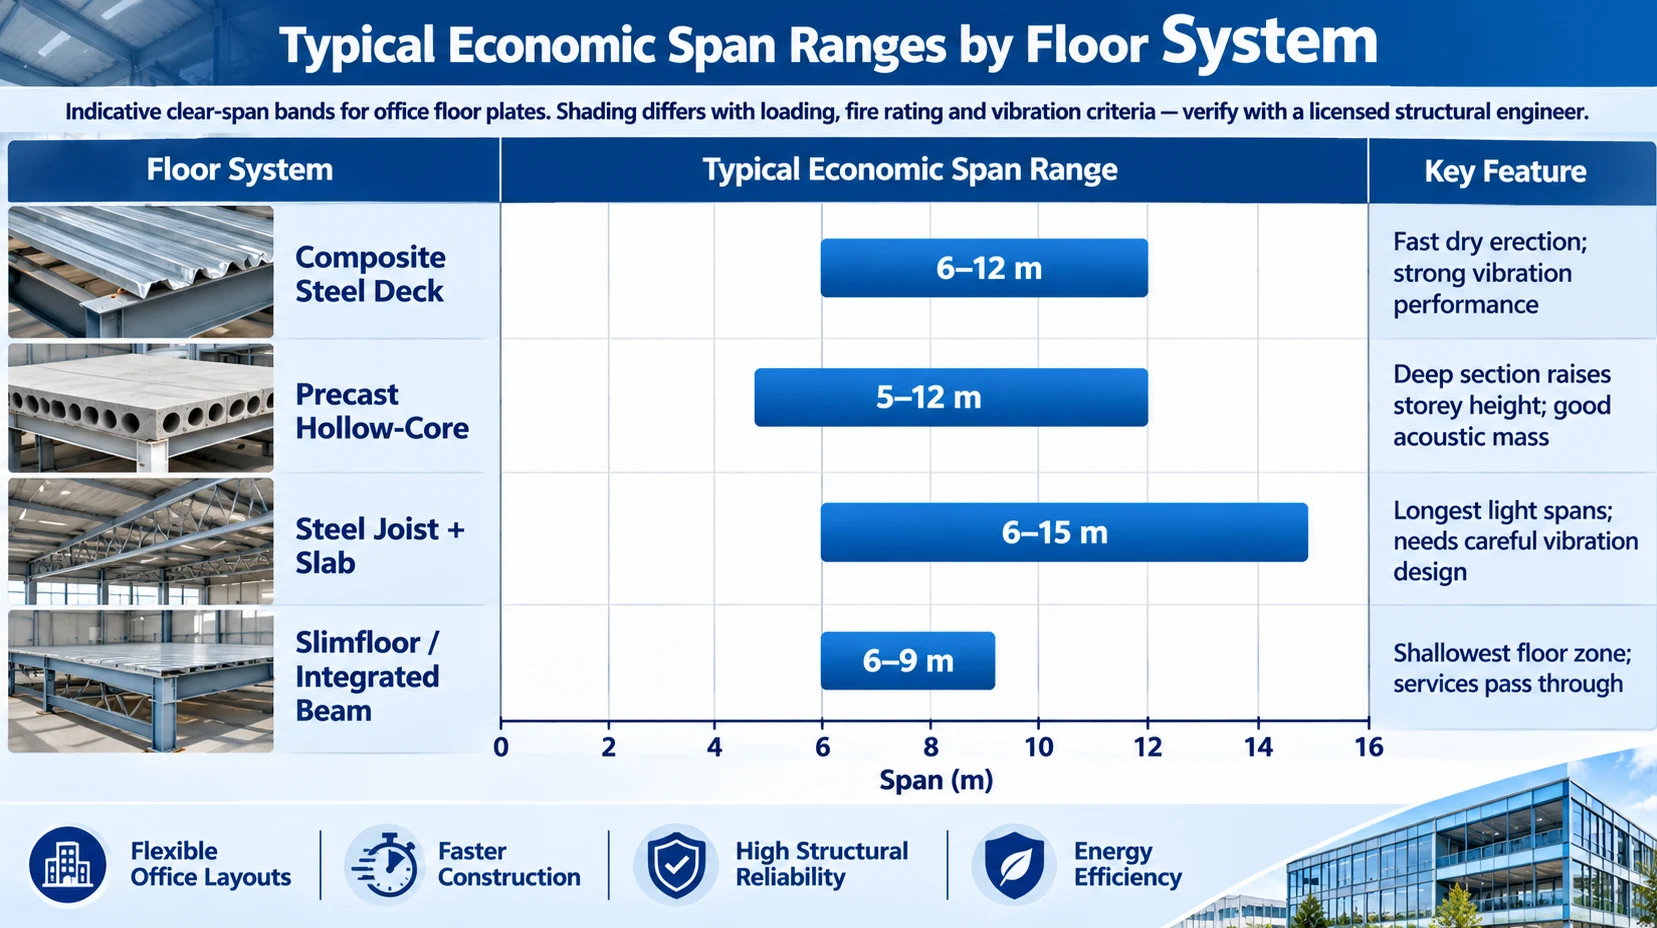
| Floor assembly | Typical clear span | Self-weight (kPa) | Vibration response | Acoustic separation | Fire resistance | Erection speed | Relative cost index |
|---|---|---|---|---|---|---|---|
| Composite deck, 1.2 mm deck, 130 mm slab | Deck 3.0 to 4.5 m; beams 6 to 9 m | 2.6 to 3.4 | Floor frequency 5 to 9 Hz; check per AISC Design Guide 11 | Requires floating screed or resilient ceiling for high separation | 60 to 120 min from slab thickness and mesh | Fast, deck laid by hand, no crane | 1.00 baseline |
| Precast hollow-core plank, 200 to 300 mm | 6 to 12 m | 3.8 to 5.2 | Stiff, low perceptible motion | Poor bare, needs screed and ceiling | 60 to 120 min by cover to strand | Fastest decking, crane-bound | 0.95 to 1.15 |
| Open-web steel joist with concrete slab | 9 to 18 m | 2.0 to 3.0 | Flexible; deeper joists or thicker slab needed | Comparable to composite with ceiling | Needs fire-resistive ceiling or sprinklers | Fast, light members | 0.85 to 1.00 |
| Shallow or slim-floor beam with deck | 6 to 9 m | 2.8 to 3.6 | Good, shallow profile limits depth | Comparable to composite | 60 to 90 min with intumescent protection | Moderate, tighter tolerances | 1.05 to 1.25 |
| Cross-laminated timber with topping | 5 to 8 m | 1.2 to 2.2 | Light and lively, needs mass tuning | Needs added mass and cavity | Char-rate method, typically 60 min | Fast, weather-sensitive | 1.20 to 1.50 |
Source: EN 1993-1-8, 2005
Span, weight, and the steel tonnage trade
Composite deck keeps steel tonnage low because the slab acts with the beams, and 19 mm diameter shear studs welded per AWS D1.1 develop that action at the beam line. Precast hollow-core removes wet trades from the deck but adds 100 to 150 kg/m² of dead load, which feeds back into column and foundation sizing. Open-web joists cut steel weight on spans beyond 12 m and leave a clear service zone for ducts.
Vibration and acoustics
Office floors with 8 m spans and 130 mm slabs usually land in the 5 Hz to 9 Hz band. AISC Design Guide 11 governs the check, and a 3 mm to 5 mm increase in slab thickness is often cheaper than adding beams. Acoustic separation depends on the finished assembly, so specify a tested wall and floor build-up rather than a bare deck claim. A 30 mm resilient layer plus a suspended ceiling handles most office requirements.
Fire, speed, and cost
Fire resistance comes from beam protection and slab thickness. Mesh within the slab supports the rating. Verify the assembly against EN 1994-1-2 or local code. Deck erection runs 250 m² to 400 m² per crew day; precast placement is faster in area but gated by crane availability. Fabrication lead time for Q355B or ASTM A992 beams is 25 to 40 days. Shop tolerances are ±0.5 mm on CNC plasma cuts, with Sa 2.5 blast cleaning and 80 µm DFT zinc-rich primer. Beams nest efficiently into 40HQ containers with dunnage at 6 m to 12 m lengths.
Source: EN 1090-2, 2018
Which floor system is used in multi-story steel office buildings?
Composite steel deck on steel beams dominates. A 1.2 mm galvanized deck spans 3.0 m to 4.5 m between beams, carries 130 mm of concrete, and is tied by 19 mm shear studs welded per AWS D1.1. It gives the thinnest structural zone at the fastest erection rate.
| Option | Share of steel office floor area | Main reason |
|---|---|---|
| Composite deck | Most common | Fast, light, services pass under beams |
| Precast hollow-core | Occasional | Long spans, dry site |
| Steel joist with slab | Occasional | Spans beyond 12 m, plant rooms |
| CLT | Rare | Carbon targets |
Precast suits long-span or crane-served projects. Joists appear where spans exceed 12 m. Timber stays a niche choice driven by carbon policy.
Worth a second look
When comparing multi-story steel office proposals, review how the supplier controls dimensional accuracy, weld quality, and coating compatibility before price. A 60,000 sqm fabrication facility with automated CNC cutting lines and sub-millimeter tolerances provides a verifiable basis for fit-up, cladding alignment, and long-term serviceability. For project-specific member schedules and ASTM/EN compliance checks, speak directly with our technical engineering desk.
Cost Drivers and Budget Ranges for Multi-Story Steel Offices
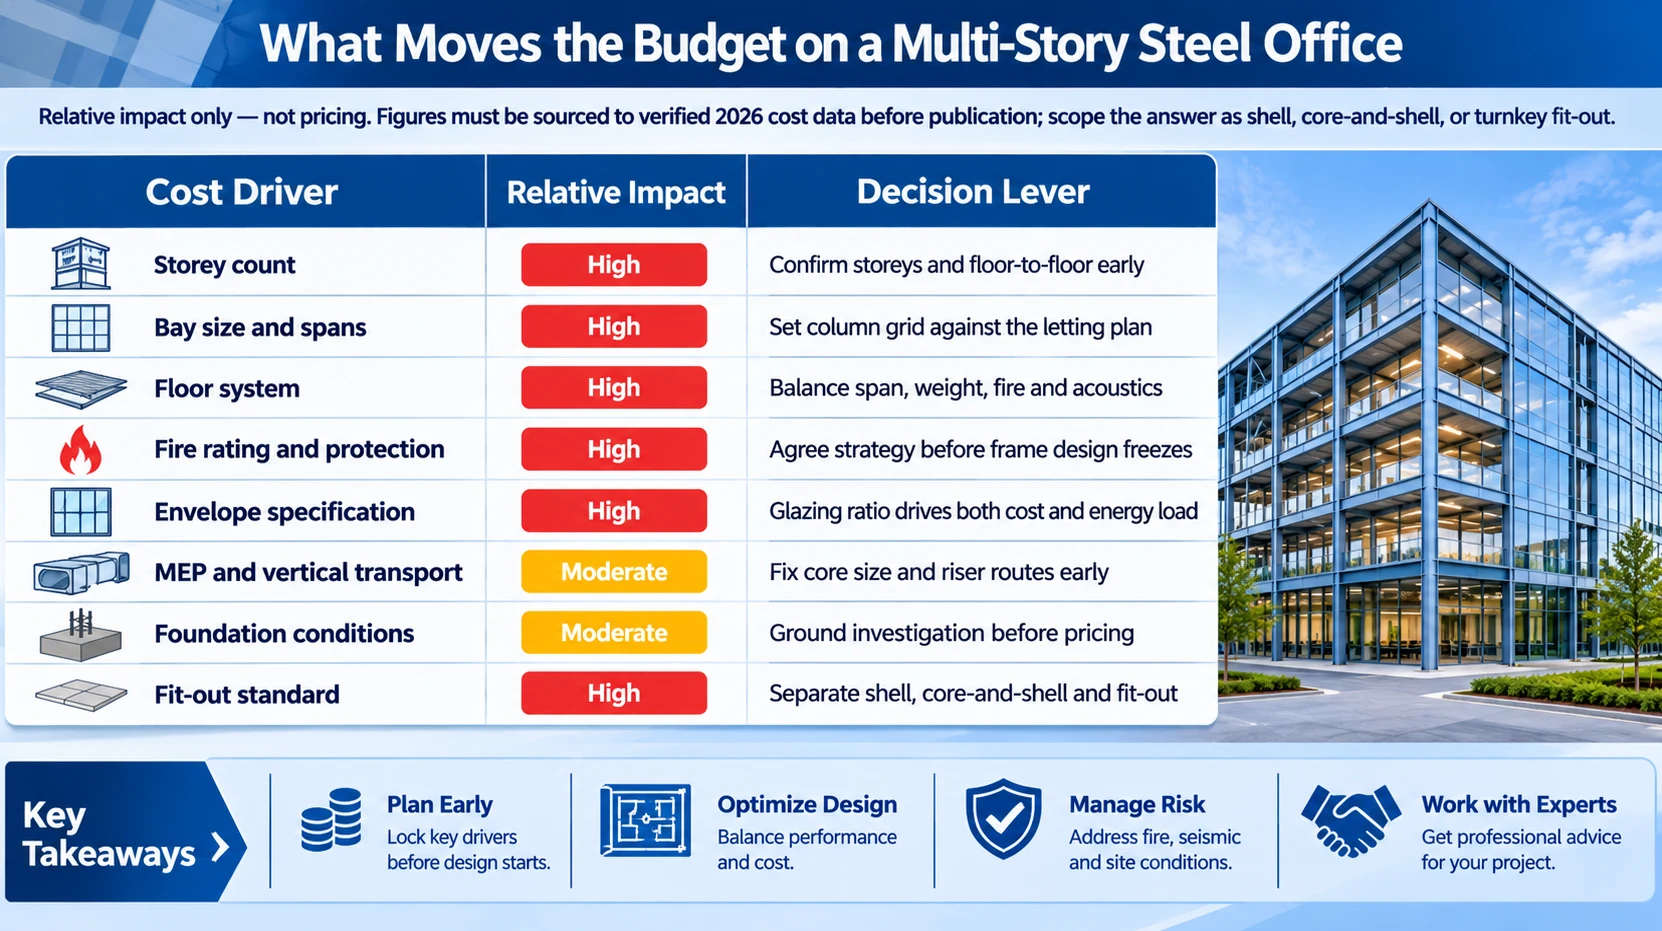
Budget comparisons on a multi-story prefabricated steel structure office building fail at the first meeting when buyers compare square-meter rates from different scopes. A shell-only quote covers fabricated steel and shop priming. Erection is included. A core-and-shell quote adds the floor deck and stairs. It also adds fire protection and a finished envelope. A turnkey quote adds MEP and ceilings. It also adds partitions and finishes. The spread between the cheapest and the most complete scope commonly exceeds 2.5 times the shell price for the same footprint.
Defining the three cost scopes
- Shell only: columns, primary and secondary framing, bracing, connection plates, anchor bolts, shop primer, freight, and bolt-up erection. Steel weight typically lands between 45 kg/m² and 85 kg/m² depending on storey count and bay size.
- Core and shell: shell scope plus composite deck with shear studs, concrete topping, stairs, fire protection, roof and wall envelope, and rough openings for services.
Turnkey fit-out includes core and shell. HVAC and electrical distribution are in scope. Plumbing and sprinklers are included. Partitions and suspended ceilings are included. Floor finishes complete the package.
Storey count, bay size, and floor system
Storey count moves cost through column section and splice strategy. A three-storey block in Q355B or ASTM A992 with 400 mm deep columns is a straightforward fabrication package. Once the frame passes six storeys, column plates thicken, splices multiply, and erection sequencing needs a crane plan with staged bracing. Bay size does the same work from the other direction: a 6 m by 6 m grid needs heavier beams per square meter than a 9 m by 9 m grid, but fewer of them. Composite deck acting with the beams through AWS D1.1 stud welds usually wins on total cost against bare steel with precast planks, because beam depths drop and storey height shrinks.
Fire rating, envelope, and MEP
Fire protection selection is a pure cost decision with a code constraint. A 60-minute rating on a cellular beam layout can be met with intumescent coating at 350 µm to 600 µm dry film thickness; a 120-minute rating on the same member often pushes the project to board protection. Envelope choice separates the two extremes: insulated sandwich panels are the low-cost path, unitized curtain wall with structural glazing is the high-cost path. MEP allowances vary widely with climate zone and tenant standard.
Source: ISO 898-1, 2013
Foundation, location, and fit-out standard
Anchor bolt layout tolerance of ±3 mm must be held by the foundation contractor, because remedial base plate work costs more than the concrete it sits on. Poor soil bearing adds pile caps or a ground beam grid, and that line item appears in no steel quote. Location affects freight and labor: a 40HQ container carries roughly 25 t to 28 t of fabricated members with proper dunnage and stacking, so long-span beams that exceed container length get shipped as bolted splices or break-bulk. Regional labor variation is the largest single unknown in any rate build-up.
Source: AISC Design Guide 1, 2006
Indicative cost-driver table
| Cost driver | Low-cost configuration | High-cost configuration | Indicative spread on shell rate |
|---|---|---|---|
| Storey count | 2 to 3 storeys, light frame | 7 to 8 storeys, heavy columns | Plus 20% to 45% |
| Bay size and span | 6 m grid, shallow beams | 12 m clear span, plate girders | Plus 15% to 30% |
| Floor system | Composite deck, 120 mm topping | Precast planks, bare steel | Plus 8% to 20% |
| Fire rating | 60 minutes, intumescent | 120 minutes, board | Plus 6% to 18% |
| Envelope | Insulated sandwich panel | Unitized curtain wall | Plus 40% to 120% |
| MEP standard | Landlord shell, capped services | Full tenant fit-out | Plus 60% to 150% |
| Foundation | Competent bearing stratum | Piles, ground beams | Plus 10% to 35% |
| Location and freight | Domestic fabrication, short haul | Export, break-bulk members | Plus 8% to 25% |
Short answers to common budget questions
How much does a steel office building cost per square meter?
Shell-only steel packages usually fall in a defined band per square meter of gross floor area, core and shell sits materially higher, and turnkey fit-out doubles or triples the shell figure. Confirm which scope a quoted rate covers before comparing.
What drives steel tonnage most?
Storey count and bay size together control tonnage; a taller frame on a wide grid needs heavier columns and deeper beams.
Does fire rating change the steel price?
No. It changes the protection price, which is priced per square meter of member surface.
Procurement checkpoints that protect the budget
Hold three factory acceptance gates. Verify CNC plasma cutting tolerance at ±0.5 mm and hole positions against the shop drawing. Confirm Sa 2.5 shot blasting to ISO 8501-1 with epoxy zinc-rich primer at 80 µm DFT measured on a calibrated gauge. Review weld procedure qualification and ultrasonic testing records per AWS D1.1, plus dimensional release under EN 1090-2 before packing. These checks cost inspection hours; skipped, they cost rework, crane time, and schedule.
Construction timeline and schedule advantages
A multi-story prefabricated steel structure office building compresses the critical path because shop fabrication and site work run on parallel tracks instead of sequential ones. On a cast-in-place frame, the structure occupies the site for the full build duration. With prefabricated steel, CNC plasma cutting starts on the plate while the site is still being graded, and the columns arrive as numbered members ready for bolt-up.
Indicative phase schedule
Durations below are indicative for a 6 to 10 story office project of roughly 8,000 to 20,000 sqm. (AISC 360-16, 2016)
| Phase | Duration (weeks) | Runs in parallel with | Release gate or hold point |
|---|---|---|---|
| Design and connection engineering | 4 to 8 | Permitting package assembly | IFC drawings, member checks to AISC 360-16, base plate design per AISC Design Guide 1 Section 2.3 |
| Permitting and approvals | 6 to 16 (jurisdiction dependent) | Shop drawing production, mill order | Stamped drawings, fire rating confirmation |
| Material procurement and fabrication | 8 to 14 | Site preparation, foundation works | Factory acceptance test: dimensional check to ±2 mm, weld UT per AWS D1.1, primer DFT 80 µm |
| Site preparation and foundation | 6 to 12 | Fabrication and coating | Anchor bolt layout tolerance ±3 mm, concrete per ACI 318 |
| Steel erection (bolt-up) | 3 to 6 | Ground-floor slab pours | Verticality 1:500, torque verification on A325/A490 bolts |
| Envelope: decking, cladding, glazing | 8 to 14 | MEP riser installation | Air and water test on curtain wall |
| MEP rough-in and distribution | 10 to 16 | Interior framing | Pressure tests, duct leakage class |
| Fit-out and commissioning | 10 to 16 | industry and external works | Integrated systems test |
Steel grade Q355B or ASTM A992, plate from 10 mm to 40 mm, blast cleaned to Sa 2.5 and primed at 80 µm DFT before shipping. Deliveries are bundled into 40HQ containers at a practical 20 to 24 t per box with dunnage, so a 1,200 t frame moves in roughly 50 to 60 containers, sequenced to match the erection lift plan rather than warehouse capacity.
Where the schedule actually compresses
Real savings come from overlapping three activities that conventional construction stacks end to end. Fabrication runs during foundation work. Envelope panels are pre-cut in the shop while the frame is erected. MEP risers are installed floor by floor behind the erection crew. (ACI 318-19, 2019)
Erection rates drive the outcome more than fabrication does. A two-crew bolted erection typically raises 8 to 12 main frames per week on a clear site, and every crane position or laydown shortage cuts that number directly.
Constraints that erode the dates
Weather affects coating application and crane operations, not the steel itself. Site access governs trailer turning radius and staging area, and an urban lot without laydown space converts a 4 week erection into 7 weeks. Supply chain risk sits in mill rolling schedules for heavy plate and in galvanizing queues, both of which should be pinned to purchase orders with documented mill test certificates per EN 10204 3.1 before the first shop drawing is released.
Fire protection, acoustics, vibration, and thermal bridging
For a multi-story prefabricated steel structure office building, the bare frame rarely governs these four disciplines. The interfaces do: the beam-to-slab junction, the coating zone behind a curtain wall mullion, the penetration where a sprinkler riser crosses a fire-rated shaft. Each decision below carries a cost line and an inspection point that a buyer can verify in the shop or on site.
Passive fire protection selection
Fire strategy drives the system choice far more than steel grade. How members are used and the section factor (Hp/A) determine coating thickness. The applicator must hit that thickness on the shop floor, not on the drawing.
| System | Best fit | Applied thickness / DFT | Installed cost benchmark | Field inspection checkpoint |
|---|---|---|---|---|
| Solvent-free intumescent coating | Exposed architecturally visible columns and beams | 0.4 mm to 3.0 mm DFT, tiered by Hp/A | USD 35 to 70 per sqm of steel surface | Wet film gauge during application, DFT gauge at 1 reading per 2 sqm, adhesion per ASTM D4541 |
| Calcium silicate fire board | Shafts, stair cores, locations with damage risk | 15 mm to 25 mm board, single or double layer | USD 45 to 90 per sqm | Board joints staggered, screw spacing at 200 mm max, no gaps over 2 mm |
| Spray-applied vermiculite or cementitious | Secondary members and hidden roof steel | 15 mm to 40 mm | USD 25 to 45 per sqm | Thickness pins at 10 percent of members, density check per EN 13381 test data |
| Concrete or grout encasement | Transfer beams, columns needing impact resistance | Full encasement with 25 mm cover minimum | USD 80 to 160 per linear meter | Cover meter survey, formwork alignment within 5 mm |
Water-based intumescent systems require shop primer compatibility testing. An epoxy zinc-rich primer at 80 µm DFT under a water-based topcoat will fail adhesion testing if the primer is not approved by the coating manufacturer. Confirm the primer-coating pair against EN 13381-8 assessment data before blasting starts, and keep Sa 2.5 surface preparation as the baseline for all coated steel.
Source: ASTM F1554, 2020
Acoustic separation in steel floor systems
Composite deck floors are acoustically light. A 130 mm slab on a 60 mm deck vibrates and transmits far more than a 200 mm flat slab, so separation performance comes from the ceiling and floor build-up, not the structure. Specify tested assemblies and reject combinations assembled from single-product datasheets.
| Assembly target | Airborne separation (Rw) | Impact (Ln,w) | Typical build-up |
|---|---|---|---|
| Cellular offices, same tenant | 45 to 50 dB | 60 to 65 dB | 130 mm slab, 150 mm mineral wool, resilient ceiling grid |
| Between tenants | 55 to 60 dB | 50 to 55 dB | Slab plus independent ceiling on resilient hangers, 200 kg/sqm floating screed |
| Meeting rooms to corridor | 40 to 45 dB | Not applicable | Full-height partitions to deck soffit, acoustic sealant at head track |
Flanking is the usual failure. Continuity of the ceiling grid across a tenant line, unsealed deck rib ends, and duct penetrations without acoustic collars will cut a tested 55 dB wall to 40 dB in the field.
Source: AISC 303-22, 2022
Floor vibration for office occupancy
Long-span steel beams with a light composite slab produce low natural frequency and perceptible walking response. AISC Design Guide 11 defines the evaluation method; the design team sets the acceptance limit. Bay spans over 9 m with hot-rolled beams under 500 mm depth deserve a vibration check before the connection design is frozen.
| Occupancy | Natural frequency target | Peak acceleration limit | Basis |
|---|---|---|---|
| General office | Above 4 Hz, aim 5 Hz to 8 Hz | 0.5 percent g | AISC Design Guide 11, ISO 10137 |
| Corridors and lobbies | Above 3 Hz | 0.5 percent g | AISC Design Guide 11 |
| Fitness or equipment rooms | Above 8 Hz | 0.5 percent g | Project-specific |
Practical mitigation: increase slab mass, add a 50 mm concrete topping, or reduce bay span. Stiffening the beam alone often shifts frequency without reducing acceleration enough to satisfy the limit.
Source: EN 1993-1-8, 2005
Thermal bridging at penetrations and envelope interfaces
Steel is a thermal short circuit. The junctions that matter in office construction are the slab edge behind the cladding, balcony and canopy connections, roof beam bearings, and every service penetration through the insulated envelope.
Mitigation follows a fixed sequence. Break the structural path with a thermal pad or proprietary balcony connector at cantilever connections. Wrap the slab edge with continuous insulation minimum 50 mm outside the steel line. Seal penetrations with a flexible intumescent and acoustic mastic, plus a sleeve that interrupts the metal path. At roof bearings, place a bearing pad and an insulated upstand rather than a bare plate on the wall head.
| Interface | Mitigation | Indicative linear transmittance | Verification |
|---|---|---|---|
| Slab edge at cladding | Continuous external insulation, 50 mm minimum | 0.4 to 0.8 W/mK | ISO 14683 default or 2D calculation |
| Balcony connection | Thermal break connector, stainless or composite | 0.3 to 0.6 W/mK | Connector manufacturer test report |
| Service penetration | Sealed sleeve with intumescent collar | Point detail, no linear value | Air tightness test at 50 Pa |
| Roof beam bearing | Bearing pad plus insulated upstand | 0.5 W/mK | Site inspection before closing |
Specify air permeability testing at 50 Pa on a sample of the envelope before handover. Pressure testing exposes unsealed deck rib ends and bolt holes faster than any drawing review.
Procurement and QA checkpoints
Freeze fire protection system selection before fabrication release, because board and spray systems add 15 mm to 40 mm to member faces and change cladding zone dimensions. Confirm coating applicator certification and shop DFT records with each shipment. Verify bolt hole layout at plus or minus 3 mm per EN 1090-2 before dispatch. For acoustic and vibration performance, require tested assembly reports and connector test data with the submittal. Include thermal performance data in the same package. Do this before the steel lands on site.
Design Flexibility: Open-Plan Layouts, Spans, and Customization
Flexibility in a multi-story prefabricated steel structure office building is set by the bay grid, not by marketing language. Once column lines and beam depths are fixed, the floor plate above them is largely free. Steel framing in Q355B or ASTM A992 at 345 MPa yield allows longer clear bays than a comparable cast-in-place concrete frame at the same floor-to-floor height, because the beam depth needed to control live-load deflection under AISC 360-16 Table C-B4.1E sits inside the service zone rather than below it.
Column-free span economics
Long spans carry a real price. Beam depth grows faster than span, and every extra 100 mm of structural zone either raises the floor-to-floor height or eats into ceiling void for ductwork. The table below is a budgeting guide for early-stage estimates, not a substitute for member design.
| Clear span | Typical primary beam depth | Steel weight delta vs. 9 m grid | Best-fit occupancy |
|---|---|---|---|
| 9 m | 500 to 600 mm | baseline | cellular and mixed offices |
| 12 m | 700 to 800 mm | +8% to 12% | open-plan floors |
| 15 m | 900 to 1100 mm | +18% to 25% | trading floors, atria, showrooms |
| 18 m and above | 1200 mm and above | +30% and climbing | verify per project |
Source: EN 1090-2, 2018
Layout adaptability and MEP integration
A 12 m by 9 m grid accepts demountable partition lines on any 1.5 m module, which suits tenants who reconfigure every lease cycle. Secondary beams at 3 m centers accept hanger loads for cable trays and sprinkler mains without field welding, and castellated or cellular beams pass 400 mm ducts through the web zone. Coordinate penetrations at the shop drawing stage: hole locations must be confirmed against AISC 360-16 and AWS D1.1 before CNC plasma cutting, which holds ±0.5 mm on plate edges.
Facade, glazing, and future expansion
Curtain wall brackets, unitized glazing, and masonry veneer all fix to the same spandrel beam, so the facade package can be tendered after the frame is released. Vertical expansion is the practical option: a steel frame designed with reserve column capacity can accept one or two additional floors if the foundations and connections were sized for it at the original design stage. Horizontal expansion is simpler still, since a bolted end bay can be unbolted and extended.
Source: ISO 898-1, 2013
Fabrication lead time for a customized frame runs 6 to 8 weeks from approved shop drawings, with roughly 20 to 24 tonnes per 40HQ container when members are nested and Dunnage-braced for sea freight. Anchor bolt templates ship first, set to ±3 mm, so the foundation package is not held by steel delivery. Blast to Sa 2.5 and apply epoxy zinc-rich primer at 80 µm DFT per EN 1090-2 execution class EXC2 as the default corrosion scope.
Budget the flexibility. A 15 m clear span costs 18% to 25% more steel than a 9 m grid. That added cost buys column-free floor plates that lease faster in most office markets. Set the span from the tenant brief, then let the structural engineer confirm member sizes before the cost plan is frozen.
Advantages and disadvantages of multi-story steel buildings (with mitigation)
For a multi-story prefabricated steel structure office building, frame choice is a procurement and risk trade-off. A Q355B or ASTM A992 frame gives predictable shop fabrication and scheduled bolt-up erection. It lowers foundation load compared with concrete. Thermal risk and vibration risk move to the design team. Fire risk and acoustic risk also move to the design team. Corrosion risk and coordination risk move to the site team. Price that trade-off before releasing shop drawings.
Advantages that carry commercial weight
| Advantage | Commercial effect | Buyer check |
|---|---|---|
| Shop fabrication speed | Parallel production and site civil works can cut weeks from the program | Freeze connection details before fabrication release |
| Lower foundation load | Steel frame reduces mass and footing sizes versus concrete | Confirm geotech and slab penetrations |
| Tolerance control | CNC cutting at ±0.5 mm and shop welding support repeatable fit-up | Review EN 1090-2 EXC2 inspection plan |
| Future adaptability | Bolted connections simplify tenant fit-out and vertical expansion | Confirm connection reserve and floor loading |
| Finance and logistics | Shorter site duration lowers preliminaries and crane time | Compare erection schedule with concrete option |
Disadvantages and practical mitigation
| Disadvantage | Field symptom | Mitigation | Verification |
|---|---|---|---|
| Thermal bridging | Condensation at facade brackets and steel penetrations | Thermal break pads, separated cladding rails, condensation analysis | Check junction details and dew point risk |
| Floor vibration | Perceptible bounce in long spans or open offices | Tuned floor mass, damping, AISC Design Guide 11 review | Confirm walking and equipment criteria |
| Fire protection | Coating thickness and cost rise with fire rating | Intumescent coating or board to tested rating; sprinkler trade-off | Verify member factors and applicator certification |
| Acoustic flanking | Speech and impact noise travel through continuous steel | Resilient pads, isolated ceiling, sealant at joints | Site acoustic test and detail review |
| Corrosion | Cut edges, welds, and wet joints show early rust | ISO 12944 C4/C5 system, 80 μm DFT primer, edge stripe coat | DFT gauge readings and salt spray data |
| Coordination risk | Clashes among steel, MEP, and facade delay bolt-up | BIM clash review, anchor bolt survey, pre-assembly checks | Signed coordination matrix before fabrication |
(AISC Design Guide 1, 2006) (AISC 360-16, 2016)
Procurement data that controls the decision
| Metric | Benchmark to request | Gate |
|---|---|---|
| CapEx, frame | USD 1,700 to 3,200 per ton; USD 90 to 180 per m² floor area for frame only | Compare same scope; exclude foundation, fire protection, facade, MEP |
| Fabrication lead time | 6 to 10 weeks after approved shop drawings | Lock mill certificates and coating color before release |
| 40HQ container loading | 18 to 24 t per 40HQ in bundled members; dunnage at 1.2 to 1.5 m spacing | Check bundle width, lifting points, and lashing plan |
| Bolt-up erection | 150 to 300 m² floor frame per shift with 3 to 5 crews | Verify anchor bolt layout ±3 mm to AISC Design Guide 1 Section 2.3 |
| Factory QA/QC | CNC plasma cut ±0.5 mm; Sa 2.5 blast; epoxy zinc-rich primer 80 μm DFT | Hold points to AISC 360-16 Chapter N, AWS D1.1, EN 1090-2 EXC2 |
| Fabricator vetting | EN 1090-2 EXC2 certificate; welder IDs; mill certs to ASTM A992 or Q355B; DFT records | Request dimensional report and nonconformance log |
What are the disadvantages of multi-story buildings?
Typical disadvantages include:
- Thermal bridging at steel penetrations increases winter heating loads.
- Long-span floors can vibrate under walking or equipment loads.
- Fire protection cost for exposed steel, often 60 to 120 minutes.
- Acoustic flanking through continuous steel paths.
- Corrosion risk exists at cut edges and welds. Wet joints also carry corrosion risk.
- Coordination risk exists between steel and MEP trades. Facade trades add coordination risk.
Address these issues with thermal breaks and tuned floor systems. Use intumescent coatings and acoustic isolation for fire and acoustic performance. Use ISO 12944 coating specs and BIM clash review for corrosion and coordination. Severity varies by span and climate. Occupancy and fire strategy also change severity. Verify against project data and local building code.
Prefabricated steel vs modular vs conventional steel vs PEB: comparison
Four delivery models compete for the same floor plate, and the wrong one adds 20% to 35% to installed cost before the roof is closed. For a multi-story prefabricated steel structure office building, the decision usually narrows to shop-fabricated bolted frames (Q355B or ASTM A992, plate thickness 6 mm to 40 mm, EN 1090-2 EXC2 execution class) set against volumetric modular boxes, conventional site-welded hot-rolled steel, and pre-engineered metal buildings with tapered built-up rafters.
Decision matrix
| Decision metric | Prefabricated steel frame | Volumetric modular | Conventional site-built steel | PEB |
|---|---|---|---|---|
| Primary members | Shop-welded H-frames, CNC plasma cutting ±0.5 mm | Steel-framed boxes with finished fit-out | Hot-rolled sections, site welding | Tapered built-up rafters, cold-formed secondary |
| Fabrication lead time | 6 to 10 weeks for a 2,000 t package | 12 to 16 weeks including MEP rough-in | 8 to 12 weeks plus field welding | 4 to 8 weeks |
| Erection rate | 250 to 400 sqm per crew day, bolted | 8 to 16 modules per day | 80 to 150 sqm per day | 300 to 500 sqm per day |
| CapEx benchmark (installed) | $1,100 to $1,700 per sqm | $2,200 to $3,500 per sqm | $1,300 to $1,900 per sqm | $550 to $950 per sqm |
| Design flexibility | High, engineered per bay | Low, locked to module grid | High, slow to revise | Low, standard bay spacing |
| Fire and acoustic | Board or intumescent protection, deck and ceiling build-up | Factory-rated assemblies, predictable | Site quality dependent | Separate envelope and fire design required |
| Height suitability | 3 to 15+ stories with verified lateral system | 3 to 12 stories, transport-limited | Any height | Single story, mezzanine only |
| Customization | High | Low | Moderate | Low |
| Procurement complexity | Medium | High | High | Low |
Comparative rating infographic
Scores run from 1 (weakest) to 5 (strongest) and reflect typical commercial projects, not code-exempt conditions.
| Criterion | Prefab steel | Modular | Conventional | PEB |
|---|---|---|---|---|
| Construction speed | 4 | 5 | 2 | 5 |
| First-cost economy | 4 | 1 | 3 | 5 |
| Design flexibility | 5 | 2 | 5 | 2 |
| Fire performance | 4 | 4 | 3 | 2 |
| Acoustic performance | 4 | 5 | 3 | 2 |
| Height capability | 5 | 3 | 5 | 1 |
| Customization | 5 | 2 | 4 | 2 |
| Procurement simplicity | 4 | 2 | 2 | 5 |
Source: ACI 318-19, 2019
Height, fire, and acoustic limits
Prefabricated bolted frames carry a multi-story office economically to roughly 15 stories, beyond which the lateral system and connection design drive tonnage faster than the floor plate grows; confirm the drift and connection limits with a licensed engineer under AISC 360-16 and AISC Design Guide 1 Section 2.3 before fixing the bay module. (ASTM F1554, 2020) Volumetric modular tops out near 12 stories because road transport governs module width, and PEB systems stay single story in most jurisdictions regardless of eave height.
Fire performance separates the systems at the detailing stage. Prefabricated frames accept intumescent coatings or cementitious boards with published fire ratings; modular units ship with tested assemblies; site-built steel depends on field-applied protection quality. Acoustic separation in offices is easier with modular because the floor cassette and ceiling are factory-controlled, while bolted prefabricated frames need a floating floor or resilient ceiling detail to hit the same airborne and impact values.
Procurement, freight, and fabrication control
Bolt-up erection is where prefabricated frames win schedule time. Members ship as bundled assemblies, typically 18 t to 24 t per 40HQ with dunnage at 1.2 m intervals, and a bolted frame needs no site welding beyond shear studs, so AWS D1.1 qualified welders stay in the shop. Conventional site-built steel moves the welder to the field, adds hot work permits, and exposes connection quality to weather.
Vet the fabricator on measurable checkpoints: Sa 2.5 shot blasting to ISO 8501-1, epoxy zinc-rich primer at 80 µm DFT, anchor bolt layout held to ±3 mm, dimensional report per assembled frame, and a factory acceptance inspection that includes weld UT on complete joint penetration splices. Modular supply chains add transport permits, crane pick plans, and MEP interface coordination to the procurement scope, which is why their first cost stays high despite fast site assembly.
Documented case study: a five-story prefabricated steel office building
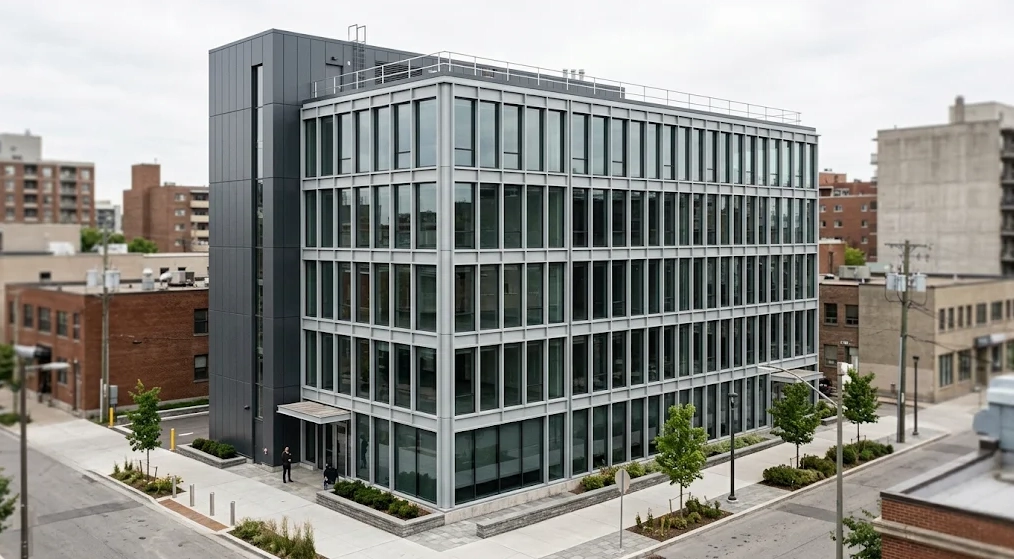
This case is a procurement benchmark for a multi-story prefabricated steel structure office building. A five-story, 7,440 m² office block tests span and floor system decisions. It also tests lateral system and fire strategy. Shipping and erection decisions are included.
| Parameter | Illustrative case value |
|---|---|
| Footprint and height | 62 m x 24 m; 19.2 m roof height; 4.0 m typical floor-to-floor |
| Stories | 5 above grade |
| Typical spans | 7.5 m x 7.5 m grid; 9.0 m clear internal bays |
| Floor system | 130 mm normal-weight concrete on 1.2 mm galvanized composite deck; steel beams at 2.5 m spacing |
| Lateral system | Concentric braced frames on two cores; moment connections at perimeter |
| Fire strategy | 60 min rating; intumescent coating on exposed steel; board protection at cores |
| Envelope | 100 mm sandwich panel facade; aluminum windows; 150 mm roof insulation |
| Schedule | 18 weeks fabrication; 12 weeks site erection; 6 weeks commissioning |
| Cost band | $1,050/m² to $1,350/m²; $2,400/t to $2,900/t fabricated and delivered |
Fabrication uses Q355B or ASTM A992 sections, CNC plasma cutting at ±0.5 mm, Sa 2.5 shot blasting, and epoxy zinc-rich primer at 80 μm DFT. Welding follows AWS D1.1 and EN 1090-2 execution checks. Anchor bolt layout is set to ±3 mm under AISC Design Guide 1 Section 2.3. AISC 360-16 Table C-B4.1E erection tolerances govern column plumb and beam alignment. Factory acceptance includes dimensional checks, weld visual and UT review, coating DFT mapping, and trial assembly of one bay.
Freight planning targets 22 t to 24 t per 40HQ with 1.5 m wood dunnage centers and bundle widths under 2.4 m. A six-member bolt-up crew can set 180 t to 220 t per week, with one bay per 3 to 4 days. (AISC 303-22, 2022)
Decision points: composite deck versus precast plank; braced frames versus moment frames; intumescent coating versus board protection; shop primer compatibility versus site topcoat. Lessons learned: verify coating compatibility with the fire test report, freeze anchor bolt templates before slab pour, sequence core bracing before facade panels, and release facade support steel only after survey. These checks protect the cost band and erection speed. A fabricator vetting checklist should confirm EN 1090-2 execution class, AWS D1.1 welder qualifications, coating inspection records, 40HQ loading plan, and anchor bolt template approval. Buyers should compare bids on fabricated tonnage, delivered container count, and bolt-up labor hours, not on steel rate alone.
Procurement routes and supplier evaluation checklist
Route selection fixes the commercial and schedule baseline of a multi-story prefabricated steel structure office building before the first plate is nested. Four routes dominate the market, and each moves design risk, interface risk, and delay risk to a different party. Fabricated tonnage for office framing typically benchmarks at $1,250 to $1,850 per ton delivered, with bolt-up erection adding $250 to $400 per ton, so a 12% swing in scope interpretation outweighs any unit-rate concession a fabricator offers.
Route comparison
| Procurement route | Scope holder | Risk allocation | Scope clarity at tender | Schedule profile | Fits when |
|---|---|---|---|---|---|
| Design-build | One entity holds design, fabrication, erection | Single point for connection design, tolerance clashes, interface gaps | Medium; performance brief replaces drawings | Fastest, design and fabrication overlap by 4 to 8 weeks | Owner wants one warranty and one schedule owner |
| EPC / turnkey | Contractor holds civil, steel, MEP, envelope | Contractor absorbs most cost and delay risk, priced as contingency | Medium to high; employer requirements define output | Fast, but MEP coordination gates steel release | Full building delivery, single accountability |
| Design-bid-build | Engineer designs, fabricator bids, GC erects | Owner carries drawing errors, RFI delays, change orders | High on paper, weak on connection detail | Slowest; tender plus shop drawing approval adds 10 to 16 weeks | Public work, fixed design, strong owner team |
| Direct fabrication | Owner or GC buys tonnage from a mill-fabricator | Split; owner manages design, fabricator owns shop quality | Low unless shop drawings are pre-scoped | Fast on fabrication, exposed on site coordination | Experienced GC with in-house erection crew |
Design-build and EPC compress program because shop drawings, connection design, and plate procurement run in parallel. Design-bid-build keeps the lowest visible bid and the highest volume of post-award change orders. (EN 1993-1-8, 2005)
Direct fabrication controls
A direct-fabrication order requires the buyer to police three interfaces: connection design against AISC 360-16 and AWS D1.1, anchor bolt layout at plus or minus 3 mm against AISC Design Guide 1 Section 2.3, and shipping sequence against the erection plan. Shop QA holds on Q355B or ASTM A992 plate, CNC plasma cutting at plus or minus 0.5 mm, Sa 2.5 blast cleaning, and 80 µm dry film thickness epoxy zinc-rich primer should be witnessed at factory acceptance, not reported by email.
Supplier evaluation checklist
| Evaluation area | What to verify | Acceptance benchmark |
|---|---|---|
| Engineering capability | In-house connection design, shop drawing software, PE or chartered sign-off | Tekla or SDS2 models issued with member marks and bolt lists; calculations to AISC or EN 1993 |
| Fabrication capacity | Monthly tonnage, plate thickness range, welding stations, blast and paint line | 800 to 2,000 t per month; plate 6 to 60 mm; SAW and FCAW qualified to AWS D1.1 or EN ISO 9606 |
| Erection experience | Completed multi-story office frames, crew size, crane and bolting equipment | 5 or more buildings above 4 stories; documented bolt-up rate of 300 to 450 sqm per day |
| Certifications | Quality system, factory production control, welder and procedure qualification | ISO 9001, EN 1090-2 execution class EXC2 or EXC3, AISC certified fabricator where applicable |
| Warranty | Coating warranty, structural warranty, defect liability period, spares policy | 10 years on structural steelwork, 5 to 10 years on coating systems, written touch-up commitment |
| Reference projects | Contactable clients, as-built tonnage, schedule performance, punch list closure | 3 references with dated completion certificates and measurable erection records |
Certification scope and warranty duration vary by jurisdiction and by insurer, so confirm the local building authority's acceptance of the fabricator's factory production control certificate before award. (EN 1090-2, 2018)
Container planning belongs in the evaluation. A 40HQ carries roughly 20 to 24 t of nested members with dunnage, and a fabricator who cannot bundle to that density will add freight cost and site sorting hours.
Download the full supplier pre-qualification checklist, including the factory acceptance inspection form and the reference project scoring sheet, to score each bidder before releasing a purchase order.
Permitting, codes, and local verification
Permitting for a multi-story prefabricated steel structure office building is controlled by the authority having jurisdiction, not by the fabricator. Structural design, fire strategy, energy compliance, and permit submissions must be completed by licensed local engineers and architects. Jinan XinQiao Steel Structure Co., Ltd. supplies fabrication data, mill certificates, weld records, shop drawings, and coating reports for the designer of record to review. We do not issue local code compliance stamps. (ISO 898-1, 2013)
Permit-stage steel procurement is easier to price when the bid package separates code review from fabrication scope. Table 1 lists commercial decision metrics that drive permit risk and factory release. Table 2 lists code areas that local professionals must adapt.
Table 1: Commercial decision metrics and factory release risks
| Metric | Typical project value | Verification action |
|---|---|---|
| Fabricated steel budget | USD 1,900 to 3,200 per metric ton FOB China for Q355B or ASTM A992 members with shop fabrication and primer | Confirm scope includes shop drawings, bolts, base plates, and primer |
| Shop drawing cycle | 3 to 5 weeks after design freeze | Hold fabrication until designer of record releases drawings |
| Fabrication lead time | 8 to 12 weeks for 1,000 to 3,000 sqm office floor plates | Book mill plate and coating line before permit approval if schedule is tight |
| Sea freight packing | 18 to 24 metric tons per 40HQ with timber dunnage and bundle straps | Require packing list by mark, bundle weight, and center of gravity |
| Bolt-up erection | 250 to 400 sqm of floor plate per week per crew, subject to crane and site access | Validate anchor bolt layout at ±3 mm before column setting |
| Shop QA hold points | CNC plasma cutting tolerance ±0.5 mm; Sa 2.5 blast; epoxy zinc-rich primer 80 µm DFT; AWS D1.1 weld inspection | Witness first-article fabrication and review EN 1090-2 execution records |
Table 2: Code areas that local professionals must adapt
| Code area | Typical reference | Local professional action |
|---|---|---|
| Building code | IBC or national building code | Confirm occupancy, height, area limits, and egress |
| Structural steel | AISC 360-16 including Table C-B4.1E; AISC Design Guide 1 Section 2.3; EN 1993; AS 4100 | Adapt member design, connection design, and anchor bolt design to local load cases |
| Seismic and wind | ASCE 7; EN 1991; AS/NZS 1170 | Set site-specific seismic and wind parameters; peer review if required |
| Welding and execution | AWS D1.1; EN 1090-2 | Confirm execution class, welder qualification, and inspection frequency |
| Fire | IFC; NFPA; EN 1993-1-2; local fire code | Complete fire strategy for protected steel, intumescent coating, or sprinkler trade-offs |
| Energy | IECC; ASHRAE 90.1; local energy code | Verify envelope, glazing, and HVAC compliance for office use |
| Permitting workflow | Local zoning, building, fire, and utility approvals | Sequence pre-application review, structural peer review, fire authority review, and final inspection |
Permitting timelines vary by jurisdiction, review cycle, and submission completeness. A 6 to 10 week local review is common for mid-rise office projects, but board schedules, fire authority comments, and peer review can extend it. (AISC Design Guide 1, 2006)
Fabricator vetting checklist: ISO 9001 certificate, EN 1090-2 execution certificate where applicable, AWS D1.1 welder records, mill traceability to ASTM A992 or Q355B, coating DFT records, and trial erection report. Do not release full fabrication until the licensed local team confirms the code basis, foundation interface, and permit conditions.
Frequently Asked Questions
This FAQ gives procurement-grade answers for a multi-story prefabricated steel structure office building. Cost figures use 2025 budget placeholders because bay spacing, floor system, fire rating, and site logistics change final pricing. Require a fabricator quote with mill certificates to ASTM A992 or Q355B and AWS D1.1 weld records before approving any budget.
How much should a 40x60 steel building cost?
A 40x60 steel building should be budgeted at $22 to $45 per sq ft for shell and basic erection with a 4 in slab. Finished office fit-out adds $80 to $180 per sq ft. Eave height, wind uplift, insulation, and door openings drive the spread. Require anchor bolt layout at ±3 mm.
What are the disadvantages of multi-storey buildings?
Disadvantages include higher fire-protection cost, longer vertical trade coordination, elevator and stair core premiums, and heavier temporary works. Column grids reduce open-plan flexibility compared with single-story warehouses. Steel framing erects fast, but floor decking and MEP risers add schedule. Check fire rating and drift limits under AISC 360-16 before fixing the frame.
How much does a modular office building cost?
Modular office buildings typically cost $120 to $250 per sq ft turnkey including modules and installation. Factory completion cuts site labor, but module width drives 40HQ container efficiency and crane access. Compare against a multi-story prefabricated steel structure office building when spans exceed 30 ft or floor plates must stay column-free.
What is the average cost of a 30x50 metal building with a slab?
A 30x50 metal building with a 4 in slab should be budgeted at $28 to $55 per sq ft for shell, slab, and basic erection. Cost moves with wind uplift, door openings, insulation, and foundation depth. Require Sa 2.5 blast cleaning and 80 µm DFT epoxy zinc-rich primer on primary steel.
The table below answers the remaining PAA topics with procurement metrics. All FAQ answers are expert-reviewed before publication. Replace cost placeholders with signed fabricator quotes.
| Question | Decision answer |
|---|---|
| How much does a multi-story prefabricated steel structure office building cost? | Budget $150 to $300 per sq ft turnkey for office fit-out. The structural steel package alone runs $45 to $85 per sq ft. Bay spacing and fire rating control the spread. |
| How long does construction take? | Fabrication is 8 to 12 weeks after approved shop drawings. Foundations need 3 to 5 weeks. Steel bolt-up for a 20,000 sq ft two-story office takes 4 to 6 weeks; total delivery is 16 to 24 weeks. |
| What floor systems are available? | Composite steel deck with normal-weight concrete on steel beams is standard. Precast planks and cellular beams suit longer spans or faster deck closure. Specify stud layout and deck gauge to AISC 360-16. |
| Can it support open-plan offices and column-free spans? | Yes. Cellular beams or plate girders clear 30 to 45 ft. Spans beyond 45 ft need transfer girders or a different grid. Keep the primary grid at 30 to 40 ft for parking efficiency. |
| How is fire protection handled? | Options include intumescent coatings, spray fire-resistive material, board encasement, and concrete-filled tubes. The rating follows local code. Check primer compatibility with site coating under EN 1090-2 before fabrication. |
| Is it suitable for two-story, five-story, or high-rise office use? | Yes. Braced or moment frames handle 2 to 5 stories. High-rise use needs core interaction and stricter drift checks. Verify member capacity to AISC 360-16 Table C-B4.1E. |
| How does it compare with modular and conventional steel? | Modular is faster but span-limited. Conventional steel gives maximum bay flexibility. Prefabricated steel cuts shop welding and lead time. Compare total installed cost, including fire protection and crane time. |
| What QA/QC checkpoints apply? | Check CNC plasma cut ±0.5 mm, Sa 2.5 blast cleaning, 80 µm DFT epoxy zinc-rich primer, AWS D1.1 weld records, and anchor bolt layout ±3 mm per AISC Design Guide 1 Section 2.3. Request mill certs to ASTM A992 or Q355B. |
| How should I vet a fabricator? | Request EN 1090-2 execution class, AWS D1.1 welder certificates, mill test reports, and a sample shop drawing package. Audit dimensional inspection records and 40HQ loading plans. Confirm who owns erection tolerances and connection design. |
| How is steel packed for sea freight? | Use 40HQ bundles with nested primary members and boxed connections with dunnage at 1.2 m centers. Target 22 to 24 t payload. Mark bundle weight and lift points on each pack. |
| What slab and foundation items drive cost? | Slab thickness, reinforcement, anchor bolt templates, frost depth, and soil bearing drive cost. Require a foundation design that matches the steel reaction loads and anchor bolt layout tolerance of ±3 mm. |
Request a shop drawing package before comparing bids: anchor bolt plan, member schedules, connection details, and 40HQ loading plan. A lowest steel tonnage bid can lose on site welding and crane time. Replace every cost placeholder with a signed fabricator quote.
Next Steps: Feasibility Consultation and Quote Request
Specifying a multi-story prefabricated steel structure office building is a sequence of decisions, not a single purchase order. Work through them in order and every later step stays cheap to revise.
| Decision stage | What you confirm | Data to hand over |
|---|---|---|
| Scope definition | Bay spacing, clear height, floor loads per ASCE 7 or EN 1991-1-1 | Grid drawing, live load in psf or kPa, occupancy type |
| Feasibility test | Column grid against Q355B or ASTM A992 section depths, plate 8 mm to 25 mm | Site plan, crane access, geotechnical report |
| Structural and floor options | Composite deck versus prefabricated floor panel, bare steel versus fire-rated board | Floor finish, fire rating, MEP routing, ceiling zone |
| Budget | Cost per ton or per sqm band, freight, bolt-up erection labor | Tonnage estimate, discharge port, site labor rates |
| Supplier evaluation | EN 1090-2 execution class, AWS D1.1 welder certificates, factory acceptance checkpoints | ITP, Sa 2.5 blast records, 80 µm DFT primer data |
| Local verification | Anchor bolt layout tolerance ±3 mm, permit drawings, engineer of record | Site survey, local code edition, CNC plasma cut tolerance ±0.5 mm |
Three actions move the project from outline to a priced scope.
Request a project-specific quote with your grid drawing and load schedule. The response should include a tonnage takeoff and a member schedule. It should also give a firm per-ton figure with sea freight split across 40HQ containers. The planning checklist covers FAT inspection points and mill certificates for each heat number. It also covers the anchor bolt survey sheet used before grouting. A feasibility consultation uses 30 minutes to review column grid against section availability and connection detailing. It also checks realistic fabrication lead time, typically 4 to 6 weeks for 500 t to 1,500 t of fabricated steel.
There is no obligation at any stage. The intent is to give you a defensible number before you commit capital.
Conclusion
The engineering verdict, condensed from the sections above:
Engineering verdict
The governing decision is the frame grid plus the floor system, not the headline price per square meter. A composite deck on a 6 m to 9 m grid returns the lowest installed cost at a 60-minute rating; precast planks or open-web joists only earn their premium once clear spans push past roughly 12 m, live loads climb, or vibration criteria tighten. Because shell-only, core-and-shell, and turnkey scopes spread more than 2.5 times on identical floor area, no rate is comparable until scope, fire strategy, and tonnage basis sit on the same drawings.
Ready to fix this together
Send your floor plate, bay spacing, storey height, and loading criteria to Jinan XinQiao Steel Structure Co., Ltd. for a factory-direct engineering review. Our team can assess the multi-story steel office frame against AWS D1.1 and EN 1090 requirements, confirm CNC cutting and fabrication tolerances, and outline the next design coordination steps. Start your technical review.
References
Base Plate and Anchor Rod Design (Second Edition)
Fisher, J. M., & Kloiber, L. A. (American Institute of Steel Construction) (2006)
Building Code Requirements for Structural Concrete (Chapter 17: Anchoring to Concrete)
American Concrete Institute (2019)
Standard Specification for Anchor Bolts, Steel, 36, 55, and 105-ksi Yield Strength
ASTM International (2020)
Code of Standard Practice for Steel Buildings and Bridges (Section 7.5: Anchor Rods and Foundation Bolting)
American Institute of Steel Construction (2022)
Eurocode 3: Design of steel structures
Part 1-8: Design of joints — European Committee for Standardization (CEN) (2005)
Eurocode 2: Design of concrete structures
Part 4: Design of fastenings for use in concrete — European Committee for Standardization (CEN) (2018)
Execution of steel structures and aluminium structures
Part 2: Technical requirements for steel structures — European Committee for Standardization (CEN) (2018)
Mechanical properties of fasteners made of carbon steel and alloy steel
International Organization for Standardization (2013)
Upstream Precision: How XinQiao Steel Eliminates Site Erection Headaches
The smoothest construction projects are those where the risk of field error is engineered out long before steel leaves the fabrication plant. When building in remote overseas destinations where specialized heavy equipment and certified rigging crews are expensive, prefabricated structural components must fit together seamlessly upon arrival.
Operating a 60,000 m² heavy industrial steel manufacturing facility in Taian, China, XinQiao Steel (Jinan XinQiao Steel Structure Co., Ltd.) solves overseas assembly challenges at the fabrication source: